

Slag inclusions are non-metallic material — solidified flux residue — trapped inside the weld. They are the signature defect of flux-shielded processes (MMA/stick, FCAW, SAW), and they most often trace back to one procedural failure: depositing a pass over slag that wasn’t fully removed.
Unlike porosity, which is rounded and volumetric, slag inclusions are often elongated and irregular — which is why acceptance standards treat them more severely: a string of slag along a fusion line behaves mechanically like a crack-like planar flaw, not like a pore. (When process control slips, defects like this form fast — watch what happens when a weld goes wrong.)
Short answer. A slag inclusion in welding is solid flux or coating residue trapped inside the weld metal or between passes, classified as reference 301 in ISO 6520-1 (reference card). It forms when a pass is deposited over slag that was not fully removed, or when the pool freezes before the slag can float out. Only processes that produce slag can cause it: stick (MMA/SMAW), flux-cored (FCAW) and submerged arc (SAW).
| Question | Short answer |
|---|---|
| What does it look like? | Inside the weld: an irregular, angular dark indication on a radiograph. At the surface: a dark line of slag at the toe or between beads |
| How is it different from porosity? | A pore is a rounded gas cavity; slag is solid, non-metallic and often elongated |
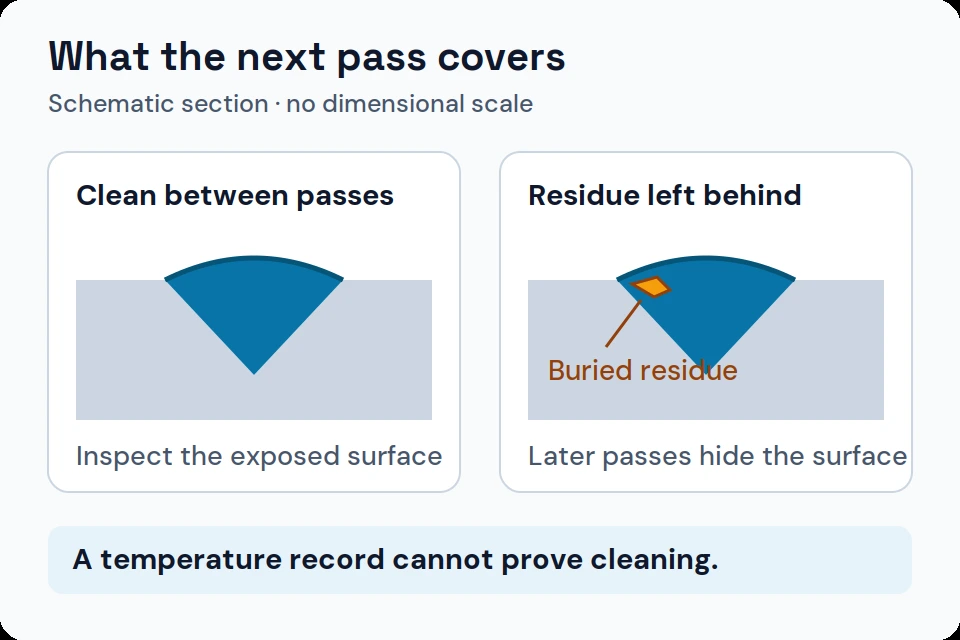
| What is the most common cause? | Incomplete cleaning between passes, especially at the toe lines of convex beads |
| Can TIG or solid-wire MIG/MAG cause it? | Not true slag. A linear inclusion in those welds points to an oxide inclusion or to lack of fusion |
| Is it always rejectable? | No. Short isolated inclusions can be within the limits of the quality level; long or aligned ones are judged more strictly |
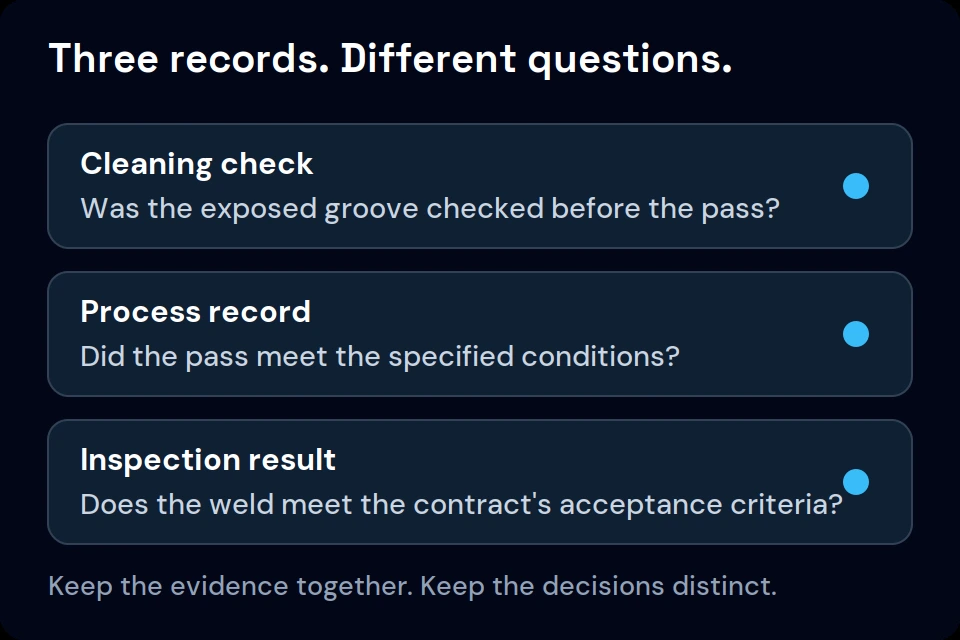
| Can it be seen while welding? | Not the trapped slag itself. Temperature records show whether the next pass started within the specified thermal window; cleaning needs its own check |
What is a slag inclusion?
ISO 6520-1 classifies solid inclusions as group 300:
| Type | ISO 6520-1 code | Description |
|---|---|---|
| Slag inclusion | 301 | Flux/coating residue trapped in weld metal (linear 3011, isolated 3012, clustered 3013) |
| Flux inclusion | 302 | Unfused flux (typical of SAW) |
| Oxide inclusion | 303 | Metallic oxide trapped during solidification (frequent in aluminium) |
| Metallic inclusion | 304 | Foreign metal particle, e.g. tungsten from TIG (3041) |
The process matters: slag inclusions are usually associated with flux processes (MMA, FCAW, SAW), and they are far less typical in gas-shielded solid-wire MIG/MAG and in TIG, which has no flux. If RT shows linear inclusions in a gas-shielded solid-wire weld, consider oxide films or lack of fusion as well, and re-read the indication before writing the NCR.
What causes slag inclusions
Interpass cleaning failures (the big one)
- Slag not fully removed between passes — particularly in the toe lines, where convex beads create a wedge the chipping hammer doesn’t reach
- Time pressure on multi-pass work: the second pass goes down while pockets of slag survive in the groove
- Difficult access (deep narrow grooves, small bevel angles) making mechanical cleaning ineffective
Technique and parameters
- Inadequate overlap between adjacent beads, which leaves a void; the next layer does not melt the trapped slag out
- Current too high combined with high travel speed, which causes sidewall undercut and makes slag hard to remove
- Electrode size or angle that does not suit the joint preparation, leaving pockets where slag collects
- Flux type: basic coatings give a more convex bead and a slag that is harder to remove from the toes, so the risk is higher in multi-pass work
Joint and surface condition
- Undercut or rough profile in the previous pass trapping slag (see undercut: causes and acceptance criteria)
- Surface oxide, rust or mill scale on the joint: slag is partly a product of the reaction between flux, air and surface oxide, so clean joint faces help
ISO 5817 acceptance criteria
ISO 5817 sets dimensional limits on solid inclusions per quality level — Level B (stringent), C (intermediate), D (moderate). The limits cap inclusion length and height as a function of material thickness, following the same logic as other volumetric imperfections: what is tolerable at Level D is rejected at Level B.
Two principles to retain:
- Isolated, short inclusions may be acceptable at intermediate levels; linear/aligned inclusions (3011) are treated far more severely because of their planar behaviour.
- Your governing code can override ISO 5817 — pressure and fatigue applications often impose stricter sentencing on linear indications regardless of level.
Exact dimensional values are in ISO 5817 Table 1 (the standard is copyrighted — keep a controlled copy at the sentencing station). For how quality levels map to your application, see the ISO 5817 guide and the B vs C vs D comparison table.
Detection
- Radiographic testing (ISO 17636) — slag shows as irregular, angular dark indications, distinguishable from the rounded form of porosity.
- Ultrasonic testing — used on thicker sections; telling slag from planar flaws depends on the procedure and the operator.
- Visual testing (ISO 17637) — catches surface-breaking slag lines at the toes, and more importantly verifies interpass cleaning before the next pass hides the evidence. A fixed welding camera can keep a dated image of the groove before each pass, which supports the hold-point record; the judgement stays with the inspector.
- In-process monitoring — a thermal record of each pass can support your quality file, but it does not identify slag: Therness has not validated slag detection (see the section below and the validation page). Overview: real-time weld quality monitoring.
Prevention checklist
- Make interpass cleaning a hold point on multi-pass WPSs — chip, wire brush or grind, with attention to toe lines and crevices.
- Aim for smooth beads with adequate overlap; avoid convex profiles and pockets that trap slag.
- Respect WPS current and travel speed: excessive current with high speed causes sidewall undercut, which makes slag hard to remove.
- Use the electrode size and angle the joint preparation calls for, so beads fuse into the sidewalls without forming pockets.
- Grind out suspect areas before the next pass: in narrow vee joints, with difficult electrodes or where slag sits under undercut, brushing or chipping may not be enough.
- Document cleaning per pass in the traveler — under ISO 3834 this is exactly the kind of in-process evidence auditors ask for.
What process monitoring can and cannot do for slag
The classical control is procedural: the WPS states the interpass temperature and the cleaning method and tool, and the welder follows it pass by pass. Interpass cleaning is checked by looking at the groove before the next pass is deposited, and the result is sentenced later by RT or UT.
Therness HeatCore records the thermal field and the electrical signals of each pass, and compares a weld with a reference weld. What it tells you today is that a weld moved away from the reference, and on which signal: “anomaly yes, defect type no”. It does not tell you that the cause is slag, and slag detection has not been measured. Our validation so far covers 4 robotic MAG and CMT welds on a linear joint with deviations induced on purpose. Manual and semi-automated welding is not validated for automatic comparison, and flux processes (MMA, FCAW, SAW) have no validation numbers. There has been no comparison with radiography, ultrasonic or destructive testing on the same welds. The details, including the limits, are on the validation page.
What in-process monitoring records on a multi-pass joint
| Record per pass | What it shows | What it does not show |
|---|---|---|
| Interpass temperature (radiometric thermal camera) | Whether the next pass started inside the specified window | Whether the groove was clean |
| Cooling behaviour between passes | Whether the pass cooled the way the qualified procedure did | Slag below the surface |
| Current, voltage and wire feed (parameter acquisition) | Whether the recorded electrical and wire-feed conditions matched the WPS; heat-input assessment also needs a separately measured travel speed and the applicable calculation | The inclusion itself |
| Thermal pattern of the pool | A pass that left its normal pattern, worth a look before the next pass covers it | A verdict: confirmation stays with VT, RT or UT |
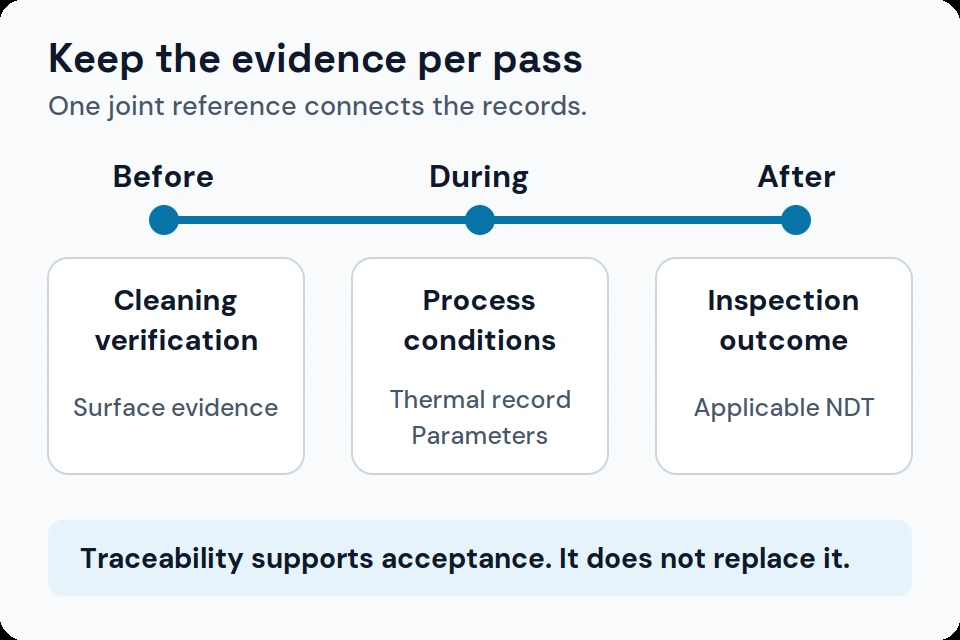
What a recording can do is add evidence to the quality file: a per-pass record that sits next to the traveler, the cleaning sign-off and the NDT report. It supports your records under ISO 3834; it does not replace the inspection or the acceptance criteria required by your customer and the applicable standards.
Slag matters most in structures and pressure equipment, where multi-pass work is dense and the consequence of a missed inclusion is high. That is also where the audit trail is most demanding: traveler, NDT records and photographic evidence of cleaning.
For flux processes and monitoring, see submerged arc welding (SAW): quality monitoring and thermal imaging and flux-cored arc welding (FCAW) quality monitoring. The welding camera hub connects camera selection to your process, HeatCam IR-S is the compact camera for robotic and embedded setups, and the comparison of weld monitoring cameras helps you choose.
Slag inclusions are one of the defects covered in our complete map: see the welding defects guide with acceptance criteria.
Keep a thermal record of every pass
HeatCore shows when a weld moves away from its reference and on which signal. It does not identify slag, and automatic comparison is validated on robotic welding today. Book a demo with our welding engineers to see what it would record on your process.
Book a demo Explore HeatCore AI monitoringTherness solution: Welding monitoring system — Each weld compared with a reference in the cycle, with anomaly flags and the ISO 3834 / ISO 17635 evidence kept per weld.
Frequently Asked Questions
What is a slag inclusion in welding?
A slag inclusion (ISO 6520-1 code 301) is non-metallic solid material — residue from electrode coating or flux — trapped inside the weld metal or between weld passes. It occurs in flux-shielded processes: MMA/stick, flux-cored arc welding, and submerged arc welding. Gas-shielded solid-wire MIG/MAG leaves mostly silicate islands and TIG has no flux, so true slag inclusions are far less typical there.
What causes slag inclusions between weld passes?
The dominant cause is incomplete slag removal before depositing the next pass, especially with convex beads where slag stays in the toe lines. Contributing factors: inadequate overlap between adjacent beads, undercut or an uneven profile on the previous pass that forms pockets, current and travel speed that cause sidewall undercut, an electrode size or angle that does not suit the joint, and a flux type (basic coatings in particular) whose slag is harder to remove.
Are slag inclusions acceptable under ISO 5817?
Small isolated inclusions can be acceptable depending on quality level; long or aligned inclusions are treated severely because they behave like planar defects. ISO 5817 limits inclusion length and height relative to material thickness, with Level B the most restrictive. Exact dimensional limits are in ISO 5817 Table 1 — verify the current edition and your governing code, which may be stricter.
How do you detect slag inclusions in a weld?
Subsurface slag inclusions are found by radiographic testing, where they appear as irregular dark indications (unlike the rounded indications of pores), or by ultrasonic testing. Surface-breaking slag at toe lines is visible in VT per ISO 17637. In production, the most effective control is procedural: enforce and document interpass cleaning before each pass is deposited.


