
Stop Guessing Weld Quality in Robotic Cells
HeatCore AI™ is a thermographic in-process weld monitoring system for robotic cells: it replaces manual checks with inline thermography and AI anomaly flags against a reference, so you catch drift early and document ISO 5817 / ISO 17635 compliance.
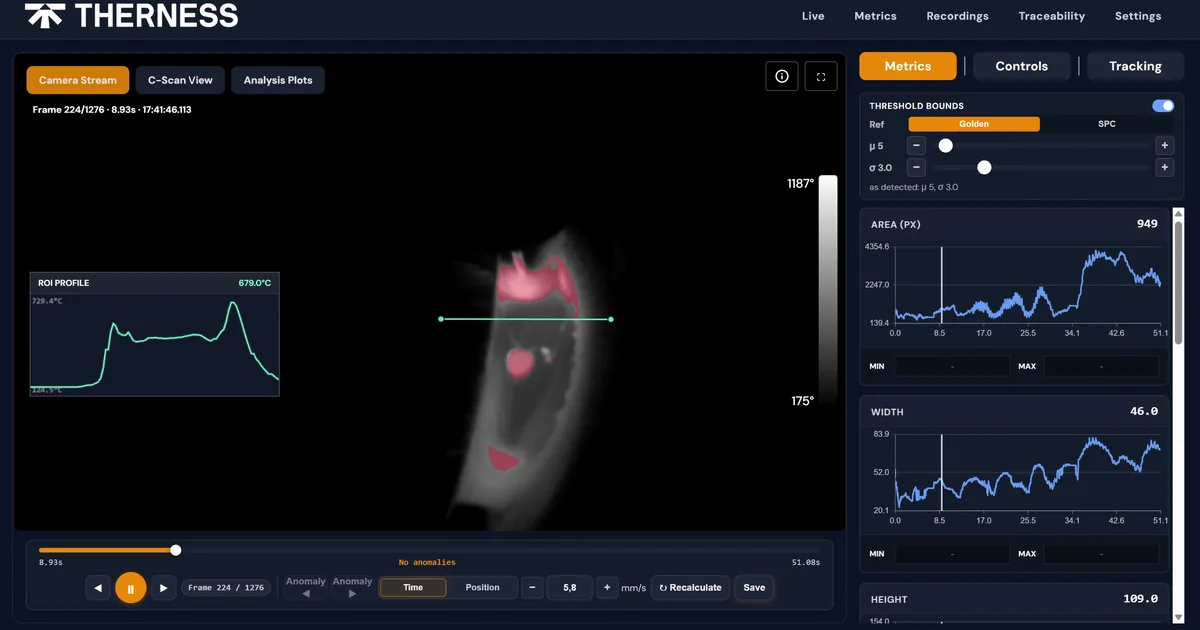
Watch the full demo
Thermal defects slip past spot checks and trigger expensive rework
Robotic weld lines move fast. Operators rarely see porosity, overheated beads, or equipment drift until parts fail final inspection.
Where things go wrong
- No continuous visibility of weld pool temperature
- Defects only found after grinding, NDT, or customer complaints
- Manual reports slow audits and root-cause analysis
The cost
- Scrap and rework eat into margins
- Robots down while teams hunt for the last good part
- Auditors chase evidence, projects miss ISO 17635 commitments
Technical guides for weld-monitoring decisions
Real-time in-process thermographic weld monitoring with defect AI
HeatCore AI™ bolts onto robotic cells, captures the weld pool with the HeatCam IR-C thermal camera at up to 25 Hz, and applies proprietary deep learning so you know which welds pass, which fail, and why. Unlike visible-light arc-visualization cameras that only show the operator the pool, HeatCore measures the weld’s thermal signature to flag heat-driven defects automatically.
Inline thermal visibility
The HeatCam IR-C (384 × 240 px LWIR microbolometer, 17 µm pitch, 8–14 µm) tracks weld pool temperature and gradients in real time.
- Range: −20 °C to 900 °C standard, up to 1500 °C optional
- Sensitivity: ≤ 60 mK NETD
- IP67 stainless-steel housing
Anomaly AI built for welding
Deep learning models and statistical pattern recognition trained on real weld data segment the weld pool and flag welds that deviate from the reference during the weld. They report an anomaly, not the defect type: see how we validate it.
- Thresholds and models validated on your own welds during the pilot
- Edge computing—no cloud dependency
- Adapts to your materials and travel speeds
Ready for MES / QMS
Feeds alarms, SPC data, and weld evidence into the Therness QMS service or your existing systems.
- REST API (OpenAPI 3.1 schema) and WebSocket; RTSP video stream
- CSV export and reports; archive on SMB, SFTP, FTP or S3
- Integration SDK (REST API, Python, C++) on project
- Bidirectional PLC integration: on project
Quality teams finally get proof, and operations keep moving
HeatCore AI is one node in a wider weld monitoring line: the same evidence packs and temperature timelines feed audits and continuous improvement.
Compliance and reporting
- Automatic evidence pack per weld pass
- Export to ISO 17635 / ISO 3834 audits in seconds
- Feeds CAPA and PPAP evidence to your QMS
Operations and ROI
- Catch defects before cutting, machining, or painting
- Fast root-cause analysis with temperature timelines
- Robots stay productive with zero extra cycle time
Inside the HeatCore AI software
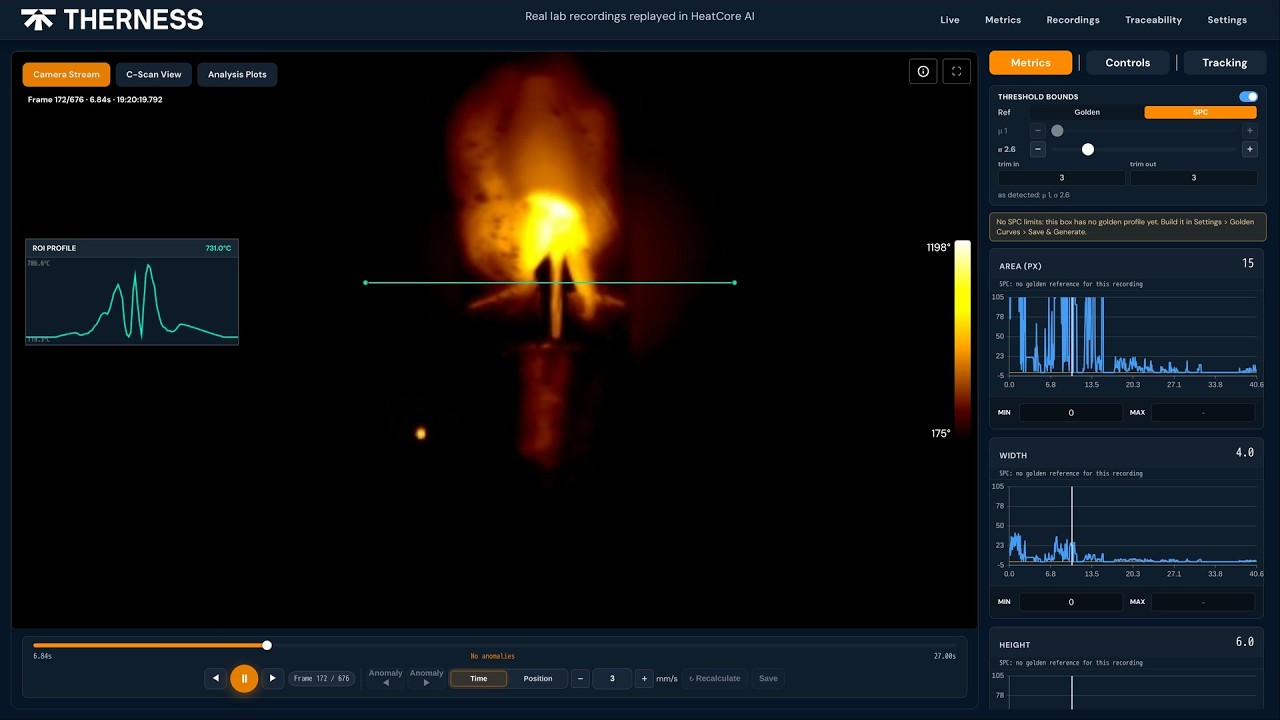
Four short screen recordings of the current software at 3840×2160. The thermal footage is the replay of one real weld from the Therness lab, reopened in HeatCore AI: not live production and not a customer line. Press play for full screen at full resolution.
HeatCore AI™: alarms, process signals and cooling time
Three clips on YouTube: a weld-pool width alarm and the Analysis Plots, both on the replay of a real Therness lab weld (not live production), and a cooling-time analysis from thermal data.


Related products
Compare HeatCore tiers and see how they fit into a full weld monitoring deployment.
HeatCore tiers
System overview
Weld Parameters module
Frequently asked questions
What defects can HeatCore AI detect?
HeatCore AI flags welds whose thermal pattern deviates from a reference learned on good welds, and process drift. It reports an anomaly, not the defect type: porosity, lack of fusion and other defect types are not classified today. Coverage depends on material, joint geometry, and acceptance criteria configured for your process.
How fast can HeatCore AI be installed on a robotic cell?
Most deployments start with a pilot cell: mount the IR sensor, align optics, calibrate emissivity/thresholds, and validate against your WPS and acceptance criteria. Timeline depends on access to the cell and the number of joint types.
Does HeatCore AI integrate with MES or QMS tools?
Yes. You can export evidence packs (PDFs) and connect alarms/metrics through the REST API (OpenAPI 3.1 schema) and WebSocket; bidirectional PLC integration is set up on project. It also feeds the Therness QMS service, which automates CAPA, PPAP and audit evidence filing.
Which standards does HeatCore AI support for documentation?
HeatCore AI is designed to support ISO 17635 / ISO 3834 evidence workflows. Final compliance requirements depend on your applicable standard, customer requirements, and inspection plan.
What is a real-time welding monitoring system for a robotic welding cell?
It is a system that checks every weld while the robot is welding, instead of sampling parts afterwards. HeatCore AI is the Therness one: an infrared sensor watches the weld and the software flags, in real time, welds whose thermal pattern deviates from a reference learned on good welds, together with process drift. It reports an anomaly, not the defect type, and builds an evidence pack per weld pass.
How do I choose a weld monitoring system for robotic welding?
Check four things: which signal it reads (thermal imaging, high-speed video of the weld pool, electrical parameters), whether it alarms during the weld or only reports afterwards, how it connects to the cell and to your quality systems, and what record it leaves for audits. HeatCore AI reads the thermal signal in real time, connects through a REST API (OpenAPI 3.1) and WebSocket with PLC integration set up on project, exports evidence packs for ISO 17635 / ISO 3834 workflows, and most deployments start with a pilot on one cell.
Scope HeatCore AI for your line
Send the joint, the process and the cell constraints. A Therness engineer replies within one business day with a deployment path, not a sales deck.
