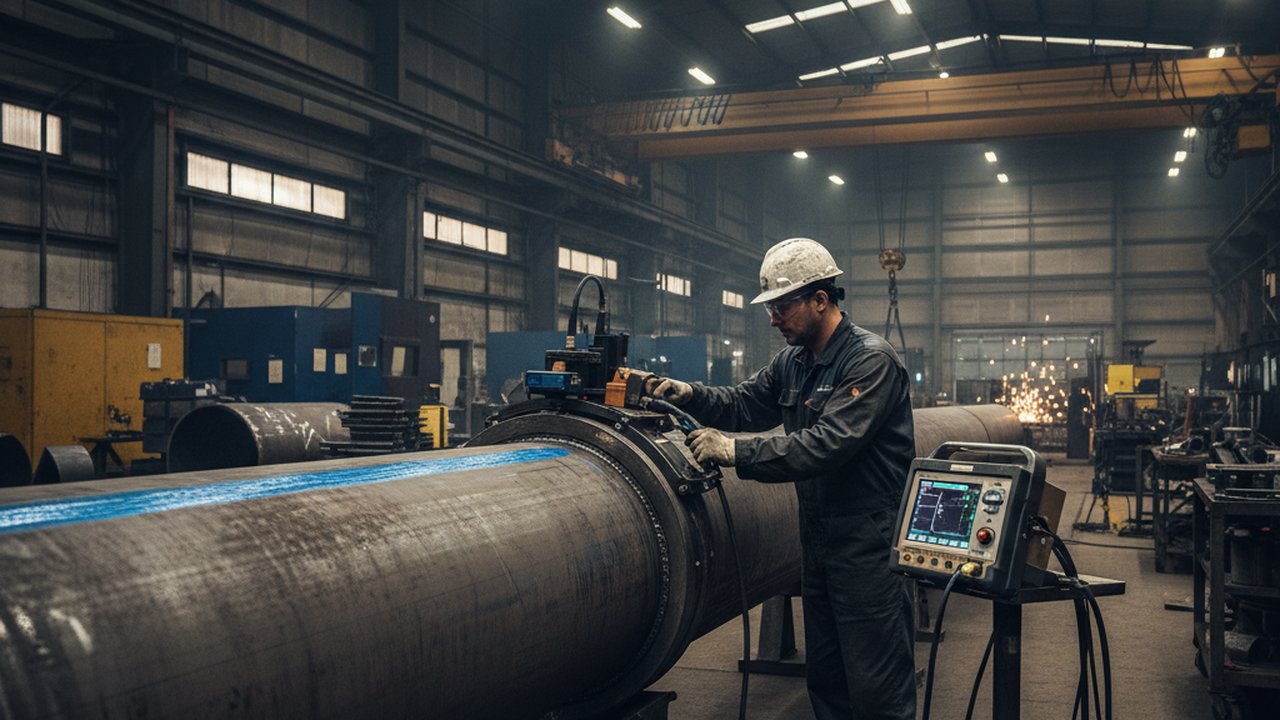
PAUT weld inspection acceptance criteria are the part of the job that decides money, and they are the part most often assumed rather than read. The scan is the easy half: a modern phased array instrument images a weld volume in one pass and hands the operator a picture. Turning that picture into “accept” or “repair” needs a chain of documents that starts in the contract and ends in the procedure — and when a fabricator and a client disagree about a reject, the disagreement is almost never about the ultrasound.
Key takeaways
- Acceptance criteria are inherited from the construction code or client specification, never written by the inspection contractor.
- Two philosophies compete: workmanship quality levels, and fitness-for-service. They give different answers about the same indication, on purpose.
- Amplitude-based and non-amplitude sizing routes are not interchangeable, and the procedure has to name one before scanning starts.
- An encoded scan is evidence; a manual scan is an observation. The difference matters at audit and in a dispute.
- Most avoidable rejects come from process drift, which is visible upstream long before an NDT technician arrives.
- If access, thickness or grain structure defeats the technique, the acceptance argument belongs to a different method.
Where PAUT acceptance criteria actually come from
The contract chain
Four documents, in order. The construction code or client specification decides what standard the weld is judged against. The acceptance standard gives the classification and the limits. The application standard says how the phased array examination is carried out so those limits are meaningful. The written procedure binds it all to your scan plan, wedges, sensitivity and personnel.
Skip a link in that chain and the argument becomes unresolvable. An indication reported without the classification rules that produced it cannot be compared against a limit, because every published limit assumes a particular way of measuring, and that is precisely what the bare report never states.
What the procedure has to fix before anyone scans
Reference sensitivity and how it was set. Wedge, probe and angle range. Scan plan and demonstrated coverage of the weld volume, including the root and the fusion faces. Encoder resolution. Classification rules for what counts as one indication rather than two. Evaluation and recording thresholds. Personnel qualification level. Every one of these changes what gets reported, and none of them is a detail.
This is also where volumetric NDT meets the rest of the quality record. Acceptance no longer rests on a single scan: welding camera footage, thermal records and parameter logs now sit beside the NDT report in the same file, answering questions the scan cannot.
If a reject is disputed, ask for the procedure and the calibration record before asking about the indication. In most disputes the disagreement resolves at the setup, not the interpretation.
Two acceptance philosophies
Workmanship quality levels
The ISO family route. Indications are classified by the phased array application standard, then judged against acceptance levels that correspond to the quality levels used for fusion-welded joints generally. The question being asked is “was this weld made to the standard of workmanship specified”, and the limits are deliberately conservative because they are not derived from the specific structure.
Fitness-for-service
The engineering critical assessment route, carried out to a recognised procedure such as the flaw assessment documents used in the pipeline and pressure equipment industries. Here the question is “will this flaw grow to failure under the loads, materials and life this component actually sees”. Acceptance limits are calculated for the job, so a flaw rejected under a workmanship level can be demonstrably acceptable — but only with fracture mechanics, real material data and a defensible loading spectrum behind it.
Amplitude and sizing
Amplitude-based acceptance compares the echo against a reference level and evaluates the length of the indication above it. Non-amplitude acceptance measures the through-wall height directly, generally from tip signals, and is what fitness-for-service work needs. Mixing them mid-job produces two incompatible datasets and a rejected inspection report.
| If the job is | Acceptance route | What it demands |
|---|---|---|
| Structural steel to a workmanship code | Workmanship levels | Qualified procedure, classification rules stated |
| Girth welds on a pipeline with an ECA in the specification | Fitness-for-service | Height sizing, material data, loading spectrum |
| Pressure equipment where the code names the standard | Whatever the construction code names | No substitution, whatever the technique can do |
| Thin section below the application standard’s scope | Another method | Radiography, or surface methods plus process evidence |
| Austenitic or dissimilar welds | Technique qualified on representative material | Demonstration blocks that reproduce the grain structure |
Building an acceptance argument step by step
- Read the contract first. Identify the construction code, the client specification and any project NDT plan, and write down which one governs when they conflict.
- Name the acceptance standard explicitly in the procedure, with its edition. “To code” is not a criterion.
- Confirm the technique is inside its scope. Thickness, material, joint geometry and access all bound the application standard.
- Choose the sizing route and state it: amplitude-based, or height sizing for an assessment.
- Qualify the procedure on representative blocks that reproduce the material, thickness and geometry, not a convenient calibration block.
- Demonstrate coverage with the scan plan. An uninspected volume is not an accepted volume, and it is the finding auditors reach for first.
- Record the setup with the data. Sensitivity, wedge, encoder, personnel and calibration checks travel with the scan file or the file proves nothing.
- Sentence indications against the named standard only, and record the classification reasoning alongside the accept or reject call.
- Close the loop on repairs. A repair is a new weld: it needs its own examination, and the repeat rate is a process signal worth tracking.
Failure modes and fixes
| Failure mode | What you see | Root cause | Fix |
|---|---|---|---|
| Acceptance standard never named | Disputes about every borderline call | Procedure written around equipment, not the contract | Name the standard and edition in the procedure header |
| Sizing route switched mid-project | Two datasets that cannot be compared | Amplitude for production, height sizing after a rejection | Fix the route at qualification and apply it to repairs too |
| Coverage gap at the root | Repairs found later at hydrotest or in service | Scan plan not demonstrated on the real geometry | Requalify on a representative block and re-plan |
| Reject rate spikes with no process change | Argument between fabricator and inspection contractor | Reference sensitivity reset differently by a new operator | Compare calibration records before touching the welds |
| Scan file without provenance | Rejected inspection report at audit | Data exported without procedure and calibration references | Bind the records into one package at the point of capture |
| Coarse-grain scatter read as flaws | High indication count on austenitic welds | Technique qualified on ferritic blocks | Requalify on representative material or change method |
Verifying that a PAUT result is real
Verification is the discipline of proving the answer would repeat if somebody else ran the same examination tomorrow. Four checks carry most of the weight, and all four are things an auditor can ask for on the day.
Sensitivity holds. Calibration and reference checks at the start, at intervals and at the end of the shift, with drift outside tolerance triggering re-examination of everything scanned since the last good check.
Coverage was achieved. The encoder trace, not the operator’s recollection, shows the scan covered what the plan required. Manual scanning without encoding cannot make this argument.
The classification is reproducible. A second qualified analyst re-reads a sample of files blind. Divergence is a procedure problem, not a personality problem.
The method agrees with itself. Where the specification allows, correlate a sample against a second technique. Comparative reasoning across methods is covered in the inspection methods comparison, and the radiographic acceptance route in the radiographic testing acceptance criteria guide. For the technique itself — probe physics, scan types and setup — the phased array ultrasonic testing guide is the companion piece to this one.
Audit-ready package for one weld: procedure with edition-stamped acceptance standard, personnel certification, calibration and reference block records, scan plan with demonstrated coverage, encoded raw data, the analyst’s classification notes, and the sentencing record with the repair history attached.
Cutting the reject rate upstream
Rejects fall into two families. Some are random. Most are the visible end of a process that drifted — a joint welded cold, a run that lost shielding, an interpass temperature nobody controlled. Those defects were being created hours before anyone put a wedge on the steel, and lack of fusion is the classic example, because the parameter excursion that causes it is far easier to see than the flaw itself.
That is the case for in-process evidence beside the NDT record. A welding monitoring system that scores every joint as it is made turns a weekly reject rate into a same-shift signal, and HeatCore AI exists for exactly that: thermal analysis of the pool and the cooling behind it, per joint, with the record kept. It does not replace volumetric NDT and no honest system claims to — the acceptance standard still owns the verdict. What it changes is how many welds arrive at the scan already known to be suspect, and how quickly the process gets corrected. The complementary NDT side, where thermography is the examination rather than the monitor, is covered on the thermography and NDT testing page, and the written-procedure discipline that makes any of it auditable is the same one described in the visual inspection procedure guide.
Where to read the real requirements
- ISO 13588:2019, use of automated phased array technology for ultrasonic testing of welds — the application standard: how the examination is performed and indications classified.
- ISO 19285:2017, phased array ultrasonic testing acceptance levels — the acceptance levels, tied to the classification above.
- ISO 5817:2023, quality levels for imperfections in fusion-welded joints — the workmanship quality levels the PAUT acceptance levels correspond to.
- ASME Boiler and Pressure Vessel Code — examination methods and the sections naming the acceptance standard.
- AWS D1.1/D1.1M:2025, Structural Welding Code — Steel — the American structural route, including ultrasonic provisions and qualified alternative techniques.
- CEN — for the EN edition in force in your country.
- Personnel and background: ASNT, the International Institute of Welding, the TWI job knowledge library, the NDT education resource centre.
FAQ
Who writes the PAUT acceptance criteria for a given weld? Nobody writes them fresh. The construction code or the client specification names an acceptance standard, and the PAUT procedure states how indications are classified so that standard can be applied. The inspector applies it and does not invent it.
Is a PAUT indication rejected on amplitude or on measured length? Both routes exist. Amplitude-based acceptance compares the echo against a reference level and evaluates length above it. Non-amplitude acceptance measures through-wall height from tip signals. The procedure must say which route governs before scanning.
Why do two PAUT operators sometimes reject different welds on the same pipe? Usually because their setups differ, not their judgement. Reference sensitivity, wedge and probe choice, scan coverage and classification rules all shift what is even detected. Two procedures produce two answers, and the argument is about setup.
Does a PAUT scan file count as inspection evidence on its own? Only with its context. A scan file is evidence when it carries the procedure, personnel qualification, calibration and reference block records, the scan plan and encoder data. Without them it is an image nobody can re-analyse or defend.
When is PAUT the wrong acceptance route for a weld? When geometry, thickness or material defeat it: coarse-grained austenitic and dissimilar welds scatter the beam, thin sections leave no room for a clean scan, and complex nozzle geometry blocks probe access. Another method then owns acceptance.
Can in-process monitoring reduce the number of PAUT rejects? It reduces the rejects that come from process drift rather than from chance. Thermal and parameter records show which joints were welded outside their qualified window, so repairs are pre-empted and the scan mostly confirms what was already known.
Arrive at the scan already knowing which welds are suspect
Per-joint thermal scoring turns the NDT campaign into a confirmation step instead of a discovery step, and shortens the loop between a drifting process and its correction.
See HeatCore AI on your weld mixTherness solution: Welding monitoring system — Every weld inspected in the cycle, with defect flags and the ISO 3834 / ISO 17635 evidence kept per weld.
Frequently Asked Questions
Who writes the PAUT acceptance criteria for a given weld?
Nobody writes them fresh. The construction code or the client specification names an acceptance standard, and the PAUT procedure states how indications are classified so that standard can be applied. The inspector applies it and does not invent it.
Is a PAUT indication rejected on amplitude or on measured length?
Both routes exist. Amplitude-based acceptance compares the echo against a reference level and evaluates length above it. Non-amplitude acceptance measures through-wall height from tip signals. The procedure must say which route governs before scanning.
Why do two PAUT operators sometimes reject different welds on the same pipe?
Usually because their setups differ, not their judgement. Reference sensitivity, wedge and probe choice, scan coverage and classification rules all shift what is even detected. Two procedures produce two answers, and the argument is about setup.
Does a PAUT scan file count as inspection evidence on its own?
Only with its context. A scan file is evidence when it carries the procedure, personnel qualification, calibration and reference block records, the scan plan and encoder data. Without them it is an image nobody can re-analyse or defend.
When is PAUT the wrong acceptance route for a weld?
When geometry, thickness or material defeat it: coarse-grained austenitic and dissimilar welds scatter the beam, thin sections leave no room for a clean scan, and complex nozzle geometry blocks probe access. Another method then owns acceptance.
Can in-process monitoring reduce the number of PAUT rejects?
It reduces the rejects that come from process drift rather than from chance. Thermal and parameter records show which joints were welded outside their qualified window, so repairs are pre-empted and the scan mostly confirms what was already known.