Conventional ultrasonic testing (UT) and phased array ultrasonic testing (PAUT) are often used as if they were the same inspection, and on a purchase order they can look interchangeable — both are “UT” on the line item. They are governed by different standards and chosen for different jobs. This guide covers conventional, manual, single-probe UT under ISO 17640 — the technique most weld shops mean when an inspector says “we’ll UT that joint.” If your application calls for automated scanning, sectorial beam steering, or a permanent digital record of every beam angle in one pass, the relevant standard is phased array ultrasonic testing (PAUT), which this page hands off to rather than duplicates.
What ISO 17640 covers
ISO 17640:2018 specifies techniques for the manual ultrasonic testing of fusion-welded joints in metallic materials with a thickness of 8 mm or greater that exhibit low ultrasonic attenuation, at object temperatures between 0 °C and 60 °C. It is written primarily for ferritic steel welds — the material class where sound travels predictably enough for a single-probe manual scan to give a reliable result without the sectorial processing PAUT equipment performs automatically.
The standard describes probe selection, scanning technique, calibration against reference reflectors, and how the operator records and reports an indication. It does not set acceptance criteria — that is ISO 11666, which converts a UT indication (its amplitude, length, and position) into an accept or reject call tied to a quality level. ISO 17640 answers “how do I perform the scan correctly”; ISO 11666 answers “is what I found acceptable.”
How a manual UT scan actually works
A conventional UT probe sends a single beam of high-frequency sound into the material at a fixed refraction angle — commonly 45°, 60°, or 70° for weld inspection, chosen based on material thickness and joint geometry. The beam travels through the material, reflects off any discontinuity or off the back wall, and returns to the probe, which converts the returning energy into a signal displayed against travel time on the instrument screen.
Because the beam only interrogates the material at the angle the probe is physically oriented to, the operator scans the probe back and forth across the weld and along its length in a pattern designed to cover the full volume from multiple angles — the technique is called a “skip” scan when the beam path bounces off the back wall to reach the far side of a thick joint. The operator calibrates against a reference block with known reflectors (typically flat-bottom holes or notches of standardised size) before scanning, so that a given signal amplitude on the live weld can be compared against the calibration curve — the distance-amplitude correction (DAC) curve — to judge whether a real discontinuity is present and how it compares to the calibration reflector.
This is inherently an operator-dependent technique: coverage, angle selection, and interpretation of a borderline signal all depend on the individual performing the scan, which is precisely why ISO 17640 ties execution to a qualified, certified operator rather than to the equipment alone.
Testing levels and where automated methods fit
ISO 17640 defines testing levels A, B, and C, with selection guidance given in the standard’s own annex based on the consequence of a missed defect and the service condition of the joint — a higher level requires broader probe angle coverage and more scan positions per joint, which is a cost and time decision, not a metallurgical one. Testing level D exists for special applications only and cannot be used unless a project specification explicitly calls for it: it covers testing on non-ferritic materials, partial-penetration welds, testing outside the 0–60 °C range the standard otherwise assumes, and testing performed with automated equipment.
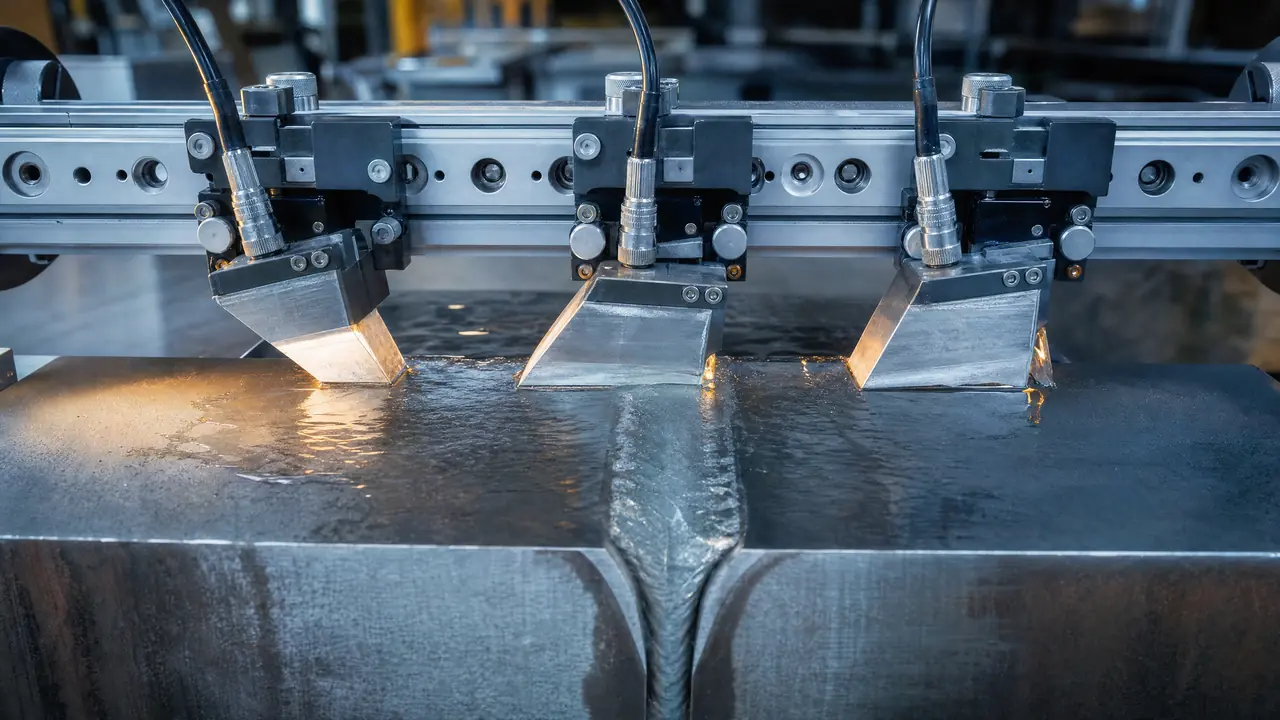
That last point is the reason PAUT and conventional UT sit in different lanes procedurally, not just technically. A phased-array system is automated scanning equipment by definition — it steers a beam electronically across dozens of angles per position rather than requiring the operator to physically re-angle a probe — so a PAUT examination is scoped under testing level D and its own procedure qualification, referencing ISO 13588 for the phased array-specific requirements layered on top of the general UT principles in ISO 17640. If your joint or your specification calls for automated scanning, start on the PAUT guide directly rather than trying to scope it under levels A–C.
Operator qualification
Both conventional and automated UT require the operator to hold current certification under ISO 9712, the international scheme for NDT personnel qualification, at Level 2 as a minimum to independently perform a scan, set up the technique, and interpret and report the result. Level 1 personnel may perform a scan under Level 2 or Level 3 supervision but do not sign off the interpretation. Level 3 personnel establish the written technique or procedure the Level 2 operator follows on a given joint configuration, and are the qualification level typically required to approve a UT procedure before it is used in production.
Conventional UT versus radiography
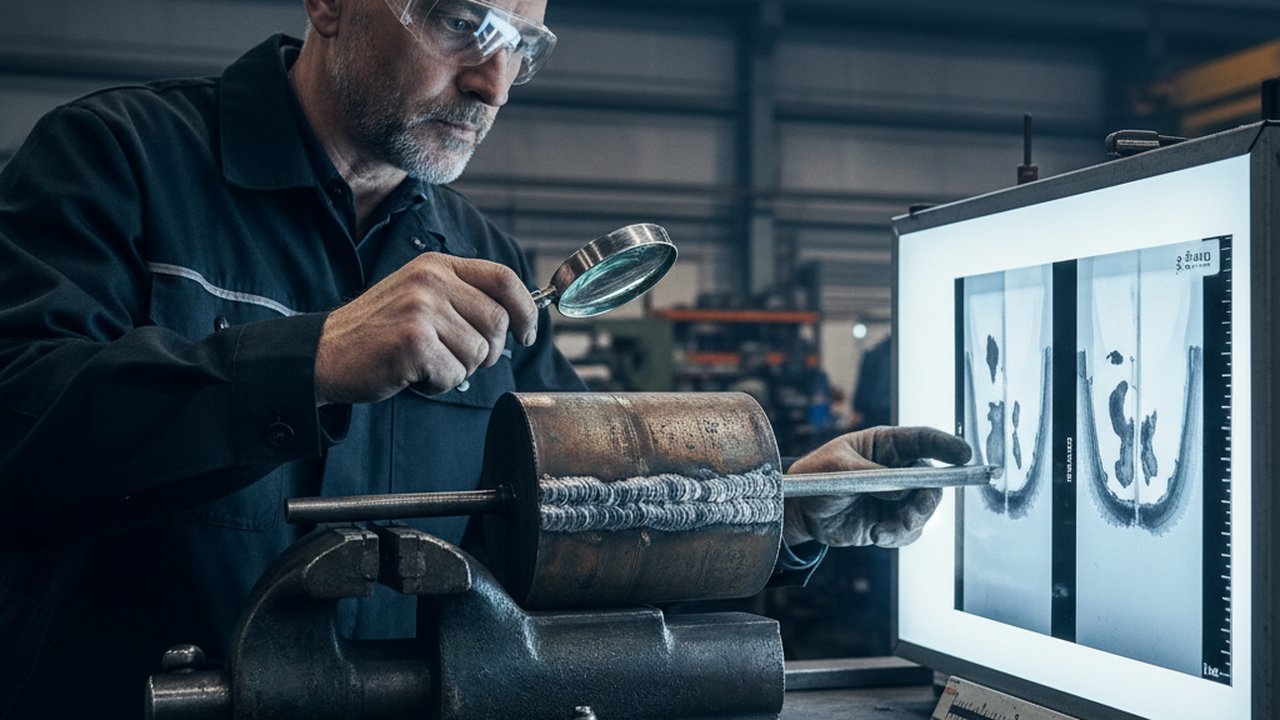
Both conventional UT and radiographic testing (RT) under ISO 17636 are volumetric methods capable of finding internal discontinuities that surface methods cannot see, and a project specification frequently allows either — or requires one over the other for a specific joint type. UT has a structural advantage that radiography does not: it is markedly more sensitive to planar discontinuities. A crack or a lack-of-fusion plane oriented across the beam path reflects sound strongly and reads as a clear indication, whereas the same planar defect can be nearly transparent to an X-ray beam travelling parallel to the defect’s plane, because radiography relies on a change in material thickness along the beam path rather than on beam reflection. Radiography, in turn, gives a permanent visual image that is easier for a non-specialist to review after the fact and is generally preferred for volumetric, rounded discontinuities such as porosity, where UT’s reflection-based signal is harder to size accurately.
Neither method requires access to only one side of the joint in the way some surface methods do, but UT requires physical probe access and adequate surface preparation (a couplant-compatible surface finish) at the scan location, which can be a constraint on complex geometries that radiography handles by positioning the film or detector on the far side of the joint instead.
Where in-process monitoring fits, and where it does not
Continuous in-process monitoring — thermal imaging of the weld pool, arc parameter recording, vision-based bead tracking — observes the welding process while the arc is open and flags conditions that correlate with defect formation. It is not a substitute for ISO 17640 examination and does not produce a UT result. A weld that shows a clean thermal and parameter record throughout the pass still requires the specified NDT if the governing code or quality plan calls for it; process monitoring supports the quality plan’s process-control evidence, it does not stand in for the confirming volumetric test. See thermographic NDT methods for where in-process observation sits relative to post-weld testing more broadly, and how the two are documented as separate evidence streams rather than one substituting for the other.
Choosing among the inspection methods
Method selection for a given weld — RT versus UT versus a surface method, and within UT, conventional versus phased array — is governed by ISO 17635, which sets out the selection logic per imperfection type and routes the extent decision to the project’s governing code. For a side-by-side comparison of how UT stacks up against visual, radiographic, and monitoring-based approaches on the dimensions that matter for a procurement or specification decision — access requirements, defect types found, documentation produced — see weld inspection methods compared.
Practical takeaways
For a welding coordinator or QA engineer scoping inspection on a new job: identify the material (ferritic steel puts you squarely in ISO 17640’s intended scope), confirm the required testing level from your governing code or ITP, and check whether the specification calls for automated equipment — if it does, or if the joint geometry demands sectorial beam angles a manual probe cannot practically cover, move to testing level D and the PAUT procedure rather than trying to stretch a manual technique to cover it. Confirm your UT operator’s ISO 9712 certification is current at the level the technique requires before the scan is scheduled, not after a report is questioned in audit. And keep the acceptance decision separate from the technique decision in your own documentation: ISO 17640 governs how the scan was performed, ISO 11666 governs whether what it found is acceptable, and a report that conflates the two is harder to defend if a customer or auditor asks which standard supports which line of the disposition.
What a UT report needs to record
A UT examination report under ISO 17640 is only as useful as its traceability back to the technique that produced it. At minimum, a defensible report records the probe angle and frequency used, the calibration reference block and reflector size the sensitivity was set against, the scan pattern applied (longitudinal along the weld axis, transverse across it, or both, depending on the discontinuity orientations the procedure targets), and for each reported indication its location along the weld, its estimated length, its signal amplitude relative to the calibration curve, and the disposition against the applicable acceptance standard. A report that states only “UT performed, no rejectable indications” without recording the technique parameters gives an auditor nothing to verify the examination actually covered the joint the way the procedure specified.
This documentation burden is also where digital and automated systems earn real value even on projects using conventional manual UT for the examination itself: a parameter and process record from in-process monitoring during welding, combined with the UT technician’s own scan record, gives a fabricator two independent, time-stamped evidence streams for the same joint — one showing the process stayed in procedure while the weld was made, the other confirming the finished joint’s internal condition. Neither replaces the other in the audit trail; together they are more defensible than either alone.
Common scoping mistakes
Three mistakes recur when a specification or an inexperienced coordinator scopes UT into a quality plan. First, assuming conventional UT and RT are freely interchangeable for any defect type — they are not; a spec that mandates RT for a joint where the governing risk is planar (lack of fusion, cracking) is asking for the wrong tool, and the reverse is equally true for rounded, volumetric porosity. Second, assuming ISO 17640 applies below its stated 8 mm thickness threshold or outside its 0–60 °C temperature scope without checking whether the actual material and conditions require testing level D or a different standard entirely. Third, treating “UT” on a specification as automatically meaning phased array capability — a supplier quoting conventional manual UT to a spec that actually requires automated scanning and permanent digital archiving of the scan data is not meeting the requirement, even though both examinations are colloquially “UT.”
Getting the technique-versus-acceptance distinction right, the testing-level scoping right, and the manual-versus-automated distinction right up front avoids a rejected inspection report late in a project, when re-scoping and re-testing cost far more than getting the specification correct at the ITP stage.
Pair UT Results with a Continuous Process Record
See how Therness in-process monitoring documents the welding conditions behind every joint you send for UT — book a demo to see it on your own welds.
Book a demoTherness solution: Welding monitoring system — Every weld inspected in the cycle, with defect flags and the ISO 3834 / ISO 17635 evidence kept per weld.